The Art of the Factory Inspection: What to Look for During a Site Visit
Key Takeaways
• On-site factory inspections reduce mass production defect rates from over 12% to under 1.5% by exposing the discrepancies between golden samples and assembly line realities.• Moisture control is the ultimate risk-mitigation checkpoint: Acacia wood must register below 12% moisture, and natural fibers like bamboo or seagrass must register below 15% to prevent mold during maritime transit.
• B2B buyers must perform bottleneck analysis on the assembly line to verify if the factory's real throughput can meet the promised 45-day lead time.
• Physical compliance verification of BSCI, SMETA, and FSC certificates on-site prevents severe customs delays and intellectual property risks.
• Container pre-loading inspections using the 7-point check and high-absorption calcium chloride desiccants are essential to prevent container rain.
THE HARD TRUTH ABOUT FACTORY AUDITS: ELIMINATING THE SAMPLE TRAP
Factory audits reduce production defect rates from an average of 14% down to less than 1.5% by exposing the discrepancy between showroom samples and actual assembly line capabilities. Many B2B buyers fall into the trap of ordering based on pristine showroom samples. These "golden samples" are handcrafted in specialized R&D departments. They do not represent mass production reality.
When a $200,000 container of rattan baskets arrives with a 15% defect rate, the margin loss is devastating. On-site factory inspections are the only way to bridge the gap between sample quality and volume consistency. Consider a recent case study in our network. A European retailer bypassed the initial audit for a 20,000-unit order of acacia serving trays.
The factory utilized unseasoned wood to meet the tight 45-day deadline. Upon arrival in Hamburg, 18% of the trays had cracked due to rapid humidity changes. The financial loss exceeded $45,000. A simple $600 pre-production inspection would have flagged the high moisture content of the wood. The inspection is not a bureaucratic hurdle. It is a strategic risk-mitigation tool. It protects your brand equity. It ensures your delivery timelines are met. Trust, but verify. This is the golden rule of global sourcing.
RAW MATERIAL AUDITING: THE SCIENCE OF MOISTURE, CURING, AND LEGALITY
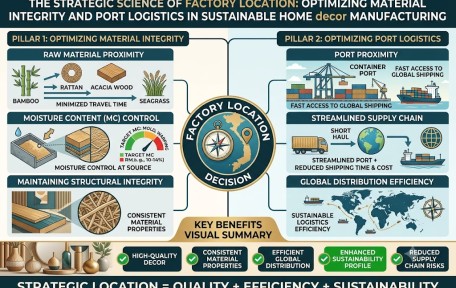
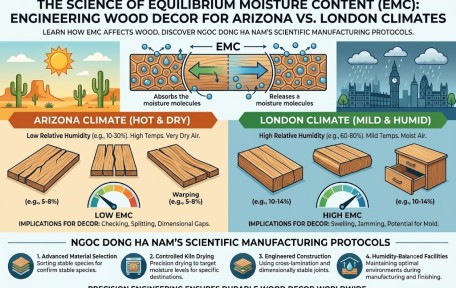
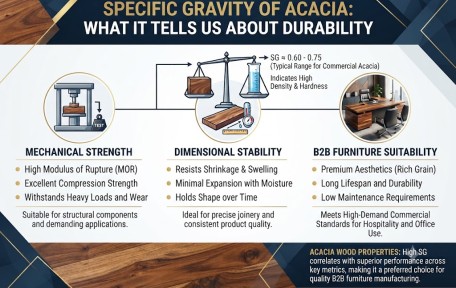
Verifying raw material quality requires testing moisture content levels—under 12% for Acacia wood and under 15% for bamboo and seagrass—directly at the storage yard. Moisture is the single greatest threat to natural fiber and wooden home decor exports. When wet wood or grass is sealed inside a shipping container for 40 days, it creates a greenhouse effect. Mold thrives. Wood warps.
During your site visit, bypass the air-conditioned boardroom. Walk straight to the raw material yard. Observe the storage conditions. Are materials stacked directly on concrete? Concrete absorbs ground moisture and transfers it to the materials. Look for elevated pallets and active ventilation.
Take out a calibrated pin-type moisture meter. Test at least 15 random planks of Acacia wood from different piles. If the average reading exceeds 12%, the wood is not sufficiently kiln-dried. For bamboo and rattan, inspect the curing process. Look for signs of powder-post beetles or fungal decay. Natural fibers like water hyacinth and seagrass must be thoroughly dried and treated. Ask to see the kiln-drying logs. A professional factory keeps meticulous records of temperature and humidity levels inside their kilns. If they cannot produce these logs, they are likely outsourcing the drying process. This introduces uncontrolled variables.
|
Material Type |
Moisture Limit |
Key Quality Indicators |
Testing Method |
|
Acacia Wood |
8% - 12% |
FSC Chain of Custody, no dead knots, uniform grain |
Pin-type moisture meter, visual grade check |
|
Bamboo |
10% - 14% |
Anti-fungal treatment, split-free nodes, uniform color |
Oven-dry method or calibrated meter |
|
Seagrass / Rattan |
12% - 15% |
Sulfur-free curing, tight weave tension, mold-free |
Resistance-type moisture probe, smell test |
PRODUCTION LINE MECHANICS: ASSESSING CAPACITY, TOOLING, AND THROUGHPUT
Bottleneck analysis on the production line is the only reliable way to verify if a factory can meet a 45-day lead time for high-volume orders. Many suppliers accept purchase orders far beyond their actual capacity. They then outsource the work to unvetted home-cottage weavers. This destroys quality consistency. To verify capacity, you must calculate the factory's actual throughput.
Walk the production line from raw material preparation to final assembly. Identify the bottleneck. In handcrafted home decor, the weaving stage is almost always the bottleneck. Calculate the takt time. If one artisan takes 3 hours to weave a single seagrass laundry basket, and the factory employs 150 weavers, their maximum daily capacity is 400 baskets. An order of 12,000 baskets will require 30 full days of production. This does not include preparation, finishing, quality control, or packaging.
Does the factory have the physical space to scale up? Look for automated machinery that can speed up preparation. CNC routers, automated sanding machines, and modern spray booths indicate high-volume capability. Ask to see the factory's master production schedule. Cross-reference it with their current order book. If their capacity utilization rate exceeds 85%, your order will face delays. Ensure they have a dedicated area for in-process inventory (WIP). Cluttered workspaces lead to physical damage and mixed-up batches.
REGULATORY COMPLIANCE: VERIFYING BSCI, SMETA, AND FSC ON THE FACTORY FLOOR
Validating BSCI, SMETA, and FSC certifications on-site prevents severe customs delays and brand damage by ensuring ethical labor and legal timber sourcing. Do not rely on PDF certificates sent via email. They are easily altered or outdated. Demand to see the original physical certificates during your visit.
Cross-reference the factory's registered business license with the address and entity name on the BSCI or SMETA audit report. Look for the DBID (Database Identifier) number. Verify its active status in real-time on the amfori or Sedex platform. Walk the factory floor to verify actual compliance. Are emergency exits clear of debris? Are fire extinguishers inspected and charged? Look at the workers. Are they wearing personal protective equipment (PPE) such as dust masks, safety glasses, and steel-toe boots in high-risk areas?
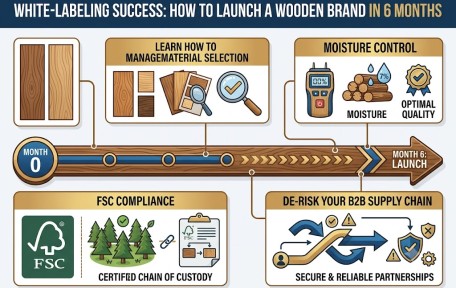
In wood processing, dust extraction systems are critical. A dusty factory floor is a severe fire hazard. It also indicates poor operational management. For FSC certification, inspect the physical separation of certified and non-certified timber. If FSC-certified Acacia is piled next to uncertified wood with no clear labels, the chain of custody is broken. Customs in Europe and North America are increasingly strict. One compliance failure can lead to your entire shipment being seized.
THE QUALITY CONTROL MATRIX: AUDITING THE INSPECTORS AND LAB EQUIPMENT
A robust factory inspection must audit the factory's internal QC processes, testing equipment calibration, and adherence to AQL 2.5 standards across raw, in-process, and finished goods. Quality control should not be a final step. It must be integrated into every stage of production. Observe the QC team in action.
How many QC inspectors are on the floor? A healthy ratio is 1 QC inspector for every 15 production workers. Ask to see their defect logbook. If the logbook is blank, they are not inspecting. Every factory makes mistakes. A real factory logs them and implements corrective actions. Check their testing equipment.
Do they have a tension testing machine for handles? Do they have a salt spray chamber for metal components? Is there a calibrated light box for color matching? Run a random cross-cut tape test on painted or lacquered surfaces. This tests coating adhesion. If the lacquer peels off easily, the finish will degrade during transit.
|
QC Stage |
Inspection Level |
Key Tests Performed |
Action on Failure |
|
Incoming (IQC) |
100% of batches |
Moisture check, dimensions, color grading |
Return to supplier or re-dry |
|
In-Process (IPQC) |
Random hourly checks |
Joint strength, weaving tension, sanding smoothness |
Stop line, recalibrate tooling |
|
Final (FQC) |
AQL 2.5 Level II |
ISTA drop test, barcode scan, function check |
100% re-inspection of the batch |
PACKAGING AND LOGISTICS SECURITY: DEFEATING CONTAINER RAIN AND TRANSIT DAMAGE
Preventing container rain and mold during maritime transit requires validating dry-packaging protocols, silica gel placement, and container pre-loading moisture checks. The journey across the ocean is brutal. High humidity and temperature fluctuations create "container rain." This moisture ruins natural fiber products.
During your inspection, review the packaging specifications. Are the master cartons double-walled corrugated cardboard (5-ply or 7-ply)? Conduct a carton drop test on-site. Drop a packed carton from a height of 30 inches (76 cm) ten times. Open the carton. If any item is broken, the packaging is insufficient.
Verify the type and quantity of desiccants used. Standard silica gel is ineffective for large containers of natural fibers. Insist on high-absorption calcium chloride desiccants. They absorb up to 300% of their weight in moisture. Before loading, inspect the container itself. Check for holes by stepping inside and closing the door. Look for light leaks. Verify the container floor moisture content. It must be below 18%. If the wooden floor of the container is wet, your cargo will absorb that moisture.
THE POST-INSPECTION PROTOCOL: TRANSLATING AUDIT DATA INTO ACTIONABLE CAPAS
The post-inspection phase must translate raw audit findings into a formal Corrective and Preventive Action (CAPA) plan with clear deadlines and assigned owners. An inspection without a follow-up is a wasted opportunity. Do not expect the factory to fix problems automatically. Categorize the findings into critical, major, and minor defects.
Critical defects (e.g., mold, structural failure, safety hazards) require immediate production halts. Major defects (e.g., wrong color tone, minor dimensional variance) require a CAPA plan within 48 hours. Minor defects (e.g., loose threads, slight packaging dust) can be monitored during routine QC. Establish a clear timeline for the factory to implement corrective actions. For example, if the kiln-drying process was found to be inconsistent, the factory must install digital temperature controllers within 14 days.
Schedule a re-inspection to verify the fixes. This systematic approach builds a culture of quality. It transitions the factory from a simple supplier to a strategic partner. Long-term supply chain resilience is built on continuous improvement.
This article is authored by Thong Nguyen – Co-owner & Sales Director at Ngoc Dong Ha Nam Co., Ltd. With 25+ years of experience managing and operating manufacturing facilities for export housewares and handicrafts, we specialize in providing high-quality bamboo, rattan, water hyacinth and natural acacia wood manufacturing solutions for global retail partners.
FREQUENTLY ASKED QUESTIONS
What is the acceptable moisture level for wood and natural fibers during inspection?
The acceptable moisture level is under 12% for Acacia wood and under 15% for natural fibers like bamboo, rattan, and seagrass to prevent cracking and mold growth during transit.
How do you verify a factory's actual production capacity?
You must conduct a bottleneck analysis by calculating the throughput of the slowest station (usually weaving or finishing) and cross-referencing it with their active workforce and schedule.
What is the standard sampling size used during a factory QC inspection?
Most international buyers use the ANSI/ASQ Z1.4 standard, commonly known as the AQL 2.5 standard, to determine the sample size and acceptable defect limits based on lot size.
How can we prevent mold during ocean shipping?
You must ensure products are dry-packaged, use high-absorption calcium chloride desiccants in the container, and verify that the container floor moisture is below 18%.